White Powder and Blueish Buckets

The temperature hovers just above freezing this morning but with wool socks, my feet are plenty warm within my steel-toed Redwing boots. The mist of Kroil stings my nostrils but that is more pleasant than the olfactory assault of a grinding wheel on steel. I can taste it all on my lips. The rattling of impact wrenches penetrates my earplugs and jars my brain. The bright orange FME covers on the open flanges provide the only contrast to the cold gray metal that surrounds me.

This combustion turbine overhaul is similar to many, but when the fuel nozzles, liners and flow sleeves come out, they are coated with a mysterious white powder.
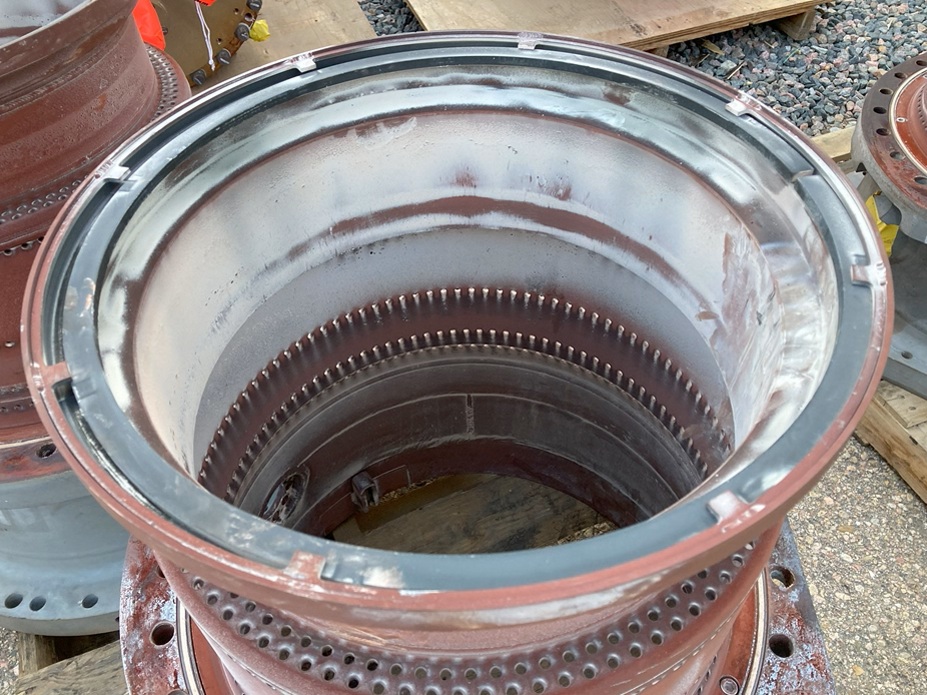
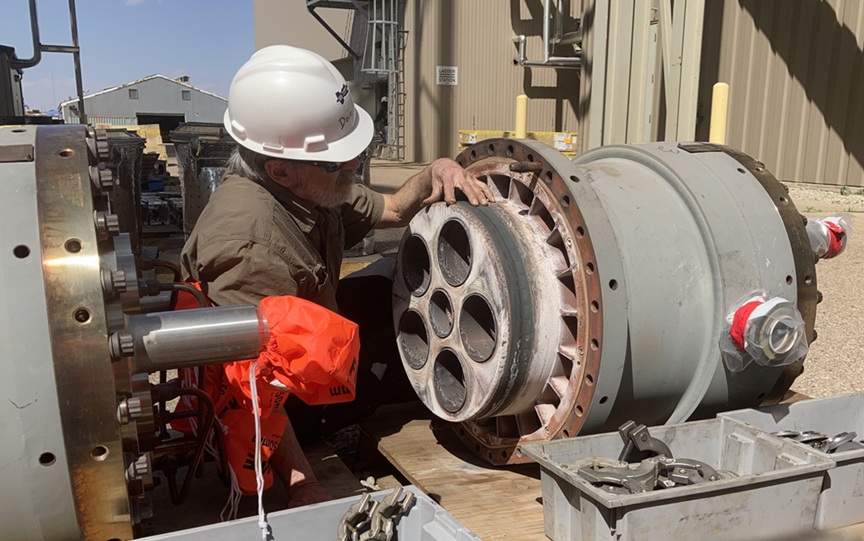
When we get the turbine case off, my eyes are immediately drawn to the blueish tint of the stage 2 buckets, and my mind rewinds to an overhaul two decades ago that exhibited a similar condition. The term “hot corrosion” comes to mind, but let’s not jump to conclusions without some help from the chemistry department and a trusted metallurgist. Their assessment confirms my suspicions.

Samples of the white powder were sent to the lab and analysis reveals that this substance is sodium sulfate[1] (Na2SO4), a corrosive salt. Bingo! My memories flash back. When this mineral gets sucked into the flame, it melts and passes through stage 1 only to condense when the temperature drops in the second stage of the turbine. This molten mineral goo can stick to the airfoils. If turbine buckets are not protected by an MCrAlY coating, the “hot corrosion” could quickly eat into the base metal and cause a catastrophic failure. Even so, this hot corrosion will eventually eat through the MCrAlY.
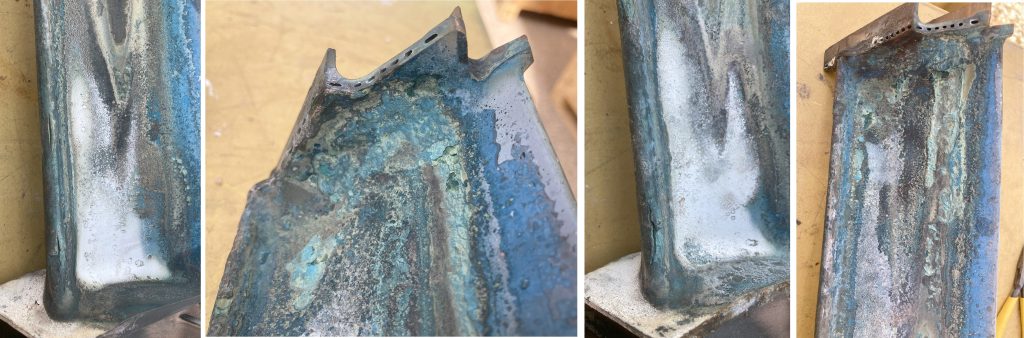
Until they are chemically stripped at the repair shop, we won’t know how compromised these buckets may have been. I suspect they will find patches with deep corrosion grooves on the surface and possibly voids beneath, but as the adage goes:

“One valid test is better than a thousand expert opinions.”

I try to chip off little samples from multiple buckets, but it is very difficult, and I have to be satisfied with a half teaspoon after much effort. The uneven splattering of these condensed minerals on the airfoils may explain why the turbine efficiency decreased in the last several months of operation.

Although the reductionist in me understands that this is sodium sulfate, I must ask “where did this come from?” My previous experience leads me up a tall ladder and into the inlet filter house. I crawl though the Hobbit door and continue to the downstream side of the evaporative cooler. As suspected, the knees of my black Carhartt jeans are now white, coated with sodium sulfate. The root cause, I believe, is high mineral content in the water used by the evap cooler combined with excessive flow which led to carryover. The high mineral water carried over to form puddles in the trough downstream of the mist eliminator and other low points, and eventually evaporated leaving the minerals behind which got sucked into the compressor and beyond.
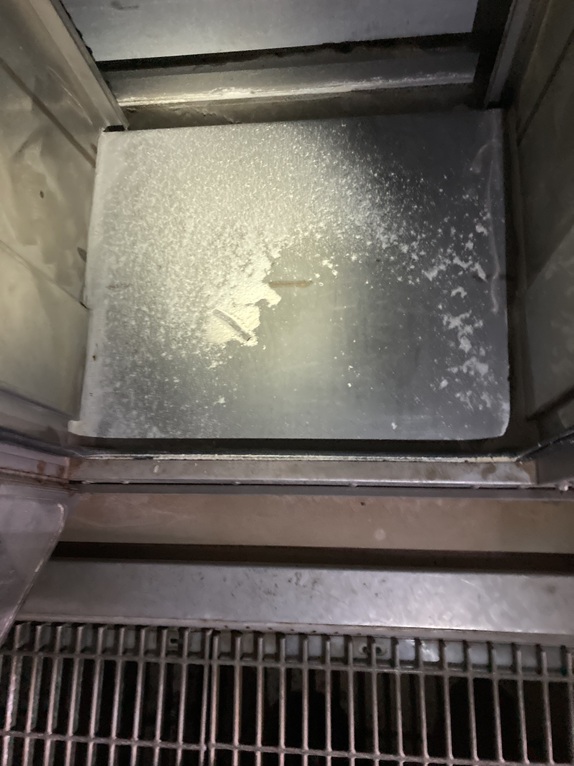
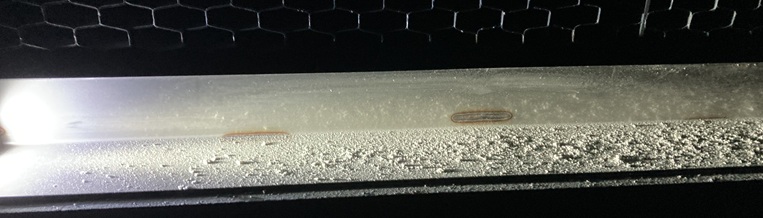
Just to be sure, I sample the powder here and compare it to what was adhered to the combustion components. It is basically the same animal… sodium and sulfur.

At this point, the logical questions are these:

  1. Can we improve the chemistry of the evap cooler water by blowing down the sump when the conductivity reaches a certain level?
  2. Can we improve the chemistry of the evap cooler water by blending domestic or well water with demineralized water?
  3. Can we reduce excess water overflow (carry-over) from the evap media and mist eliminators?

Yes, yes, and yes, but not without effort. The payback will be to preserve turbine efficiency and to reduce refurbishment or fallout replacement costs. If you need suggestions or help with 1) and 2), give me a call. And for 3), again, you can give me a call if you like. I can instruct you and/or help you commission your evap cooler when you return it to service in the spring. This is the cheapest option.

Don’t let water with high mineral content (and/or the powdered minerals it leaves behind) enter your compressor, combustion system, and turbine. The potential hot corrosion will cost you in the long run, but it can be minimized. I am an engineer, not a chemist nor a metallurgist, so if anyone with those credentials would like to add anything (or correct me), please chime in by leaving a comment below. Here is a good reference article describing the hot corrosion phenomenon:

https://www.sciencedirect.com/topics/materials-science/hot-corrosion


[1] Fun fact: The white powder form of Na2SO4 used to be known as Glauber’s salt which was used as a laxative from the mid-1600s up until the invention of Ex-Lax Milk of Magnesia and the like in the early 1900s. But please – don’t try this at your power plant.

Stranger Than Fiction

This is a story I published on my personal blog a few years ago, but it will be fun to repeat it here. But please forgive me if I “over-explain” things for this technical audience.

I am a mechanical engineer who primarily oversees work on GE 7FA combustion turbines that drive generators that produce electricity at power plants. That is my job. These units contain a large axial compressor that feeds combustion and cooling air for the gas turbine section. During a recent inspection on one of the units, we discovered damage within the compressor that required an emergency repair.

The outer case is assembled with over a hundred bolts that are approximately an inch diameter by a foot long. These are removed with the force of a hydraulic wrench and then our crane can remove the upper case which weighs over five tons. The stationary vanes in the forward part of the compressor are mounted into carrier rings that slide into a hook in the case. With significant metal-to-metal contact, rust and corrosion tends to seize these rings in place making them extremely difficult to remove. In this case, the damage is down at the bottom (six o’clock position) and we need to remove the lower rings.

If that description does not give you a mental picture, here are a couple visuals….

Open CompressorGE 7FA axial compressor with upper case removedCarrier Ring with VanesCarrier ring with stator vanes after being removed from lower half hook fit

Chemists from around the world have developed various solvents that dissolve certain types of corrosion without attacking the base metal. Some of these solvents are brushed on, some are sprayed on, some are poured into a tank and have parts dipped into them or set in overnight to soak like dishes in a kitchen sink. On this compressor, there is a narrow gap between the carrier ring and the case, and typically, various solvents or penetrating oils are poured down this gap to loosen and dissolve ring-to-case rust and corrosion. This step is necessary if there is any hope of removing these carrier rings.

I don’t want to give away too many trade secrets, but there is a solvent that is much cheaper and perhaps more effective than others. This product is also pretty useful for cleaning toilets, among other things. And… it’s the real thing.

Coca ColaCoca-Cola – “It’s the real thing”

A fact that continues to amaze me is that some people are known to voluntarily pour this powerful solvent into their mouths and down their own throat. You can’t make this stuff up. As they say, sometimes truth is stranger than fiction.

Stage 1 Nozzle Refurbishment

On many combustion turbines, certainly on the GE 7FA, the Stage 1 Turbine Nozzle is probably the most critical component for turbine performance and emissions margin. The throat area plays a big factor in the amount of hot gas flowing through the turbine, and it also plays into the compressor pressure ratio (CPR) which affects firing temperature. This component also has the potential of using too much of the precious compressor discharge air whether by excessive cooling air consumption, or bypassing this air around the chordal hinge seal.

who cares if it is round? I do.

A perfectly round nozzle ring is not necessary, but if it is out of round / elliptical by more than 1/8 inch, not only will it make transition piece installation more difficult, but it is a sign that something is wrong. It could be that the support ring itself is warped, but that is what usually gets all the attention and is not typically the problem. The horizontal joint seals may not be fully engaged, but that can be remedied. The main problem is if the duplex airfoil segments get warped (too much heat during weld repairs) and subsequently jammed into the support ring. This will warp the overall ring and could cause gaps in the chordal hinge which is supposed to seal axially against the stage 1 shroud blocks. A good after-the-fact check for this is to look at the downstream side of the used nozzle ring during an outage after a run and look for rusty-colored streaks. Those are tell-tales of a leaky chordal hinge.

throat area

Through a long series of precise measurements, the “throat” between the forty-eight stage 1 nozzle airfoils is calculated. The turbine is designed for a specific throat area. If it is too large, it will cause one type of problem, and if too small, it will cause another type of problem, both of which will affect overall turbine efficiency and MW output. There is an optimal range for S1N throat area, and your refurbishment vendor should know this target and report how close they got. If this is not a part of your repair spec, we can help.

all those little cooling holes

The stage 1 nozzle airfoil segments are cooled by compressor discharge air through ports in the outer support ring. The air passes through perforated inserts and out through small cooling holes strategically located in the airfoils and platforms. There are two circuits, one to the leading edge and one to the trailing edge. GE issued a Technical Information Letter (TIL) which describes performance issues (high NOx / low output) after installing refurbished stage 1 nozzles, and they point to excessive cooling air flow. Some vendors take this very seriously while others prefer to ignore it because it is complicated to measure and expensive to remedy. If your repair vendor does not look at this, you need to find someone who does.

What is That Freight Train Sound?

Audible Combustion dynamics

You have probably been out at your combustion turbine during a startup and heard the low-frequency rumble when the combustion system lights off. It might remind you of a passing freight train. But what about during normal operation, maybe even at base load? If you hear a similar sound then, it is likely a sign of trouble, maybe an imminent unit trip.

For those of us who grew up through the 1960s and 70s, it seemed that air conditioning was only for the luxury cars, and the rest of us kept the windows down during the summer, especially that little triangle wing vent on the front seat windows that could point air right at your sweaty neck. More recently, in this century especially, car manufacturers seem to assume that windows are never down while driving, and automobile engineers only seem to consider optimizing laminar flow for fuel economy and totally disregard the renegade motorist who may just want some fresh air. If someone rolls down your back windows on the highway, the acoustics can be horrifying.

Maybe you have kids who sit in the back seat of your car while cruising down the highway on a road trip. At some point, they may decide it would be a good idea to roll down their windows. Wump-wump-thump-thump, eardrums about to burst… “HEY!! – What do you think you are doing?!? Roll your window back up!!!” In fact, if no one is riding shotgun, the back of the passenger seat might vibrate and maybe even start bouncing around. This is similar to the low frequency acoustic dynamics that can happen inside the combustion system on your gas turbine.

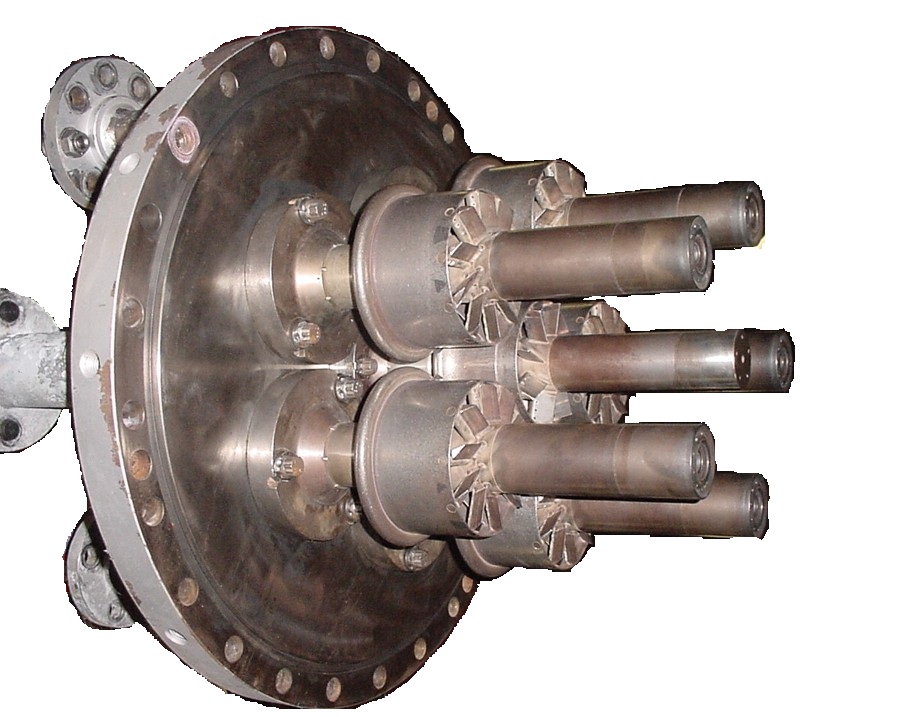
This discussion is based on GE Vernova’s DLN 2.6 combustion system, but the ideas are applicable to other systems as well.

Audible Combustion dynamics

Inherent with lean, low NOx combustion systems, acoustic dynamics develop due to a number of factors including the combustion process itself. Combustion dynamics are acoustical signatures of your flame. There is a spectrum of sound at various frequencies and monitoring these with microphones (CDMS probes) can serve as a window into your combustion process.

The type of destruction caused by the commonly defined “tones” is a topic for a different day, but you have probably heard of terms GE used to call “hot tones,” “cold tones,” “screech tones,” and “Lean Blow-Out (LBO) tones.” The complete spectrum of sound within your combustor has amplitudes that are conveniently categorized into well-defined “bins” that GE Vernova now calls “Peak 0, 1, 2, 3, ….” But be aware that these destructive “tones” only cause noticeable damage if the peak-to-peak amplitude surpasses some threshold. Unlike a passing freight train or the window-down acoustics in your car, most of these tones get drowned out by the other noises inherent with an operating combustion turbine. But when LBO / Peak 0 tones get out of hand, these are detectible with the human ear above the typical roar of your gas turbine.

These low-frequency tones are always present, but do not pose a problem if they stay below a half a psi or so. When they get up closer to 1 psi, you can hear the rumble, see circles form in your coffee cup, and this 16 Hz sound it will eventually shake the walls in the PEECC like a train is passing on an adjacent railroad track. This is about the time it will blow out your flame and trip your unit.

GE and others call this phenomenon “Lean Blow-Out” or more recently, “Peak 0 / LBO tones.” I prefer the term “chug,” which is what Mitch Cohen taught me a couple decades ago. Lean Blow-Out is a bit of a misnomer that implies that there is not enough fuel to sustain the flame. Although I readily acknowledge the mystery inherent with fire and I do not want to be dogmatic, I will state that there is probably something else going on in there besides a lean fuel-air ratio. Let’s just call this low-frequency rumble “chug.”

Consider This

Just as physical materials have natural frequencies and can be excited by adjacent vibrations (think about a tuning fork), so it is with fire. Just as high 110 Hz “Cold Tones” can crack the impingement sleeves of your transition pieces, so it is that high chug tones can wreak havoc with your flame stability and literally blow out your flame. And once one of the outer fuel nozzles in your DLN 2.6 combustion starts to increase this noise, it often excites resonance in adjacent flames from other nozzle tips. Adjacent cans can even hear it through the crossfire tubes and before you know what is going on, you hear the relays click and unit starts to spin down. Here is a short article that explains a phenomenon that combustion engineers typically may not consider: https://physicsworld.com/a/dousing-flames-with-low-frequency-sound-waves/. Try searching the Internet with “extinguishing fire with sound” and you will see a wide variety of inventions ranging from subwoofers putting out kitchen fires to wild ideas of how to sound-blast a forest fire into submission. But we want to turn all this around and consider how to prevent sound from putting out a fire that we want to be sustained… the flame within your combustion turbine.

What to do?

The low-frequency (~16 Hz) chug combustion dynamics is audible if it approaches 1 psi peak-to-peak amplitude. This resonance often occurs when the DLN 2.6 outer fuel nozzles (PM2 and PM3) are flowing very similar amounts of fuel gas. This is often called “even splits” and is the PM3 split value (nominally 60%) that produces the lowest NOx. However, once these tones become excited, they talk to each other (resonate) and can easily get amplified. It is like the table in the lunchroom at most plants. Once one person starts complaining, the negative attitude resonates with the others sitting around the table, and before long they are all complaining. So it is with your outer nozzles.

Of course, an important caveat is that “every unit is different” and some systems can sit with an “even split” all day long with no ill effects. Just as complaining can be embedded in the personality of certain individuals, so it is with particular combustion systems. Some units are very susceptible to chug and others are oblivious to it. It is the job of your combustion tuner to leave your unit with sufficient margin against all the destructive tones including the chug dynamics.

With a typical PM3 split schedule, reducing load will usually back you away from even splits, but if you are sitting at the controls and have access to the PM split schedule, ramp up the PM3 splits +1% or 2% as fast as possible. If you have a good autotune program, this is what should happen automatically. This will break up the uniformity of the outside diameter of the flame and defuse that resonant 16 Hz acoustic dynamics. To continue the analogy above, at the table in your lunchroom, it takes someone to break rank and start talking about something positive to mitigate the negative rumble. If you or your autotune software ramps up PM3, your unit might then be stuck with NOx that is higher than you like, but that is a different story and a job for a tuner who knows other knobs to help reduce NOx. But essentially, plant management might need to decide between elevated NOx verses plant reliability.

So, whatever those chug gremlins are doing inside your fuel nozzle can, this is my theory of why increasing PM3 split can pull your GE DLN 2.6 combustion system out of it.

Also, as a side note, an advantageous feature of the newer DLN 2.6+ combustion system is a pilot gas cartridge in the outer nozzles. These small diffusion flames greatly increase the chug margin to the point where it is almost a non-issue with the upgraded 2.6+.

For the Curious

Recently, out of curiosity, I subjected myself to temporary torture the other day. With a lighter perched on my thumb doing 65 MPH down the freeway, I pushed the buttons to open the rear windows. Sure enough, as the thumping noise pounding my eardrums increased, the dancing flame blew out even though it was sheltered from any breeze. Try it yourself if you care to endure some acoustic pain to your ears.

Humans have conducted substantial research about fire and flame stability and dynamics and fuel-air ratio and separating O2 from the chain reaction and other brilliant ideas that tend to make us think we have it all figured out. However, we must remain somewhat humble and acknowledge that although we are smart enough to control fire in order to produce megawatts, we may never understand everything going on in there. Fire is like a living, breathing animal. I have shared my thought process and imagination of what happens with this particular phenomenon. I welcome other ideas and would love to have some invigorating discussions about the fire inside your combustion system.